What Are Manufacturing Control Systems?
Manufacturing control systems are the operational layer that turns production plans into coordinated machine activity. A programmable logic controller can regulate a filling line; supervisory control and data acquisition software can display temperatures, speeds, and alarms. Manufacturing execution systems can connect those shop-floor signals with work orders and quality records. Together, these tools help teams monitor processes, respond to variation, and keep production consistent. The exact setup differs by plant.
Consider a conveyor carrying parts past a sensor. If spacing changes, the controller can adjust speed or alert an operator before the line backs up. That is useful, but not magic. Results depend on accurate sensors, clear procedures, and people who understand what the system is reporting. A dashboard cannot fix a poorly defined process by itself.
Industry investment reflects this growing interest. Deloitte and the Manufacturing Institute’s 2024 Smart Manufacturing and Operations Survey found that 86% of surveyed manufacturing executives viewed smart factory solutions as a primary driver of competitiveness over the next five years. The finding signals strong expectations, not guaranteed returns; survey responses are not proof that every deployment succeeds. This guide explains what manufacturing control systems include, how key components work together, and where they fit within modern production. It also considers practical limits, including legacy equipment, integration effort, and the need for reliable operational data. These details matter. A system is only as useful as the decisions it supports.
Definition and Purpose of Manufacturing Control Systems
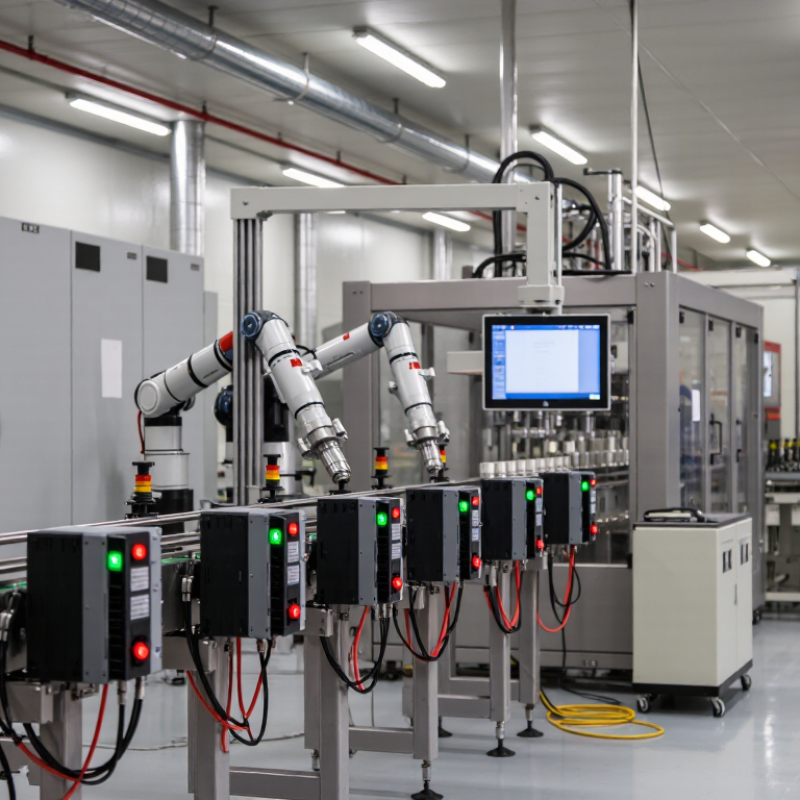
A manufacturing control system coordinates machines, people, and production data so work proceeds safely and consistently. Sensors measure conditions such as temperature, pressure, and line speed. Controllers compare those readings with set targets, then adjust motors, valves, or alarms. Higher-level software can schedule jobs, track materials, and flag quality issues. The purpose is practical: reduce variation, spot problems earlier, and give operators a clearer view of each production step.
These systems range from a single machine controller to connected plant-wide operations. The International Federation of Robotics’ World Robotics 2024 report recorded 541,302 industrial robots installed worldwide in 2023. That figure reflects growing automation, but more automation does not guarantee better control. Poorly chosen targets or unreliable sensor readings can still produce bad decisions. A dashboard may look precise while hiding a process problem. That deserves scrutiny.
Tips: Start with one measurable bottleneck, such as repeated stoppages or temperature drift. Check sensor calibration and data timestamps before trusting alerts. Keep manual procedures clear for equipment failures. Then compare results against a baseline, including downtime and rejected parts. Small gains count. A system should help operators act, not merely collect data.
What Are Manufacturing Control Systems? Definition and Purpose
A manufacturing control system coordinates equipment, processes, and production operations. The ISA-95 hierarchy below shows how control activities range from the physical process on the factory floor to business planning.
Purpose: These systems help monitor production, manage manufacturing operations, and connect shop-floor activity with business planning.
Core Components and System Architecture
What Are Manufacturing Control Systems?
Core Components and System Architecture
Manufacturing control systems connect equipment, people, and production data so a factory can monitor and adjust its processes. At the machine level, sensors measure temperature, pressure, or speed, while programmable logic controllers (PLCs) run local actions. An edge layer can filter data and coordinate nearby equipment. Supervisory control and data acquisition (SCADA) systems give operators a live view; manufacturing execution systems (MES) track work orders, quality checks, and material use. Enterprise systems handle wider planning. Historians store time-stamped readings for later analysis.
The architecture works best as a feedback loop: a sensor detects a change, a controller responds, and operators see the result. Connections between layers need clear access controls and reliable network segmentation. Deloitte and MAPI’s 2024 Smart Manufacturing and Operations Survey found that 86% of respondents expected smart manufacturing to drive competitiveness within five years. That expectation is significant, but adding software alone does not guarantee better production. A neat architecture diagram can also hide awkward handoffs between teams.
Tips: Trace one real production signal, from sensor to operator screen, before designing integrations. Note where delays or manual entries appear. The map may expose gaps that the idealized diagram misses.
How Manufacturing Control Systems Operate
What Are Manufacturing Control Systems?
How Manufacturing Control Systems Operate
A manufacturing control system gathers information from equipment and uses it to guide production. Sensors may measure temperature, pressure, speed, or the position of a moving part. A controller compares those readings with target values, then adjusts motors, valves, or other equipment. For example, if a filling line runs too slowly, the controller can change conveyor speed within defined limits. Operators monitor activity through screens that show process values, machine status, and alarms.
Small changes matter.
Some systems also record production data, making it easier to trace when a setting changed or a fault appeared. Supervisors can use those records to spot recurring delays, while technicians check sensors and equipment when readings seem unusual. The layers must communicate clearly. A sensor that drifts out of calibration can make a dashboard look precise while showing the wrong value. Too many alarms can also cause operators to overlook an important warning. Regular checks help, but they cannot replace judgment on the floor. A practical control setup gives workers useful information, clear ways to respond, and enough flexibility for real production conditions. That balance takes attention.
Common Types and Their Applications
Manufacturing control systems connect machines, operators, and production data, though their jobs differ.
A programmable logic controller (PLC) manages quick, repeatable actions. It might regulate conveyor speed or stop a press when a safety guard opens. PLCs commonly serve individual machines and compact production cells. Simple, direct control.
Supervisory control and data acquisition (SCADA) systems collect readings from equipment across a site. Operators can use a screen to spot a tank’s rising temperature or a stalled line.
Distributed control systems coordinate many connected processes, often in continuous production such as food processing or chemical manufacturing.
Manufacturing execution systems (MES) track work orders, material use, and production quality between the factory floor and business planning tools.
The boundaries can blur. A smaller plant may combine functions, while a larger facility may separate them.
Real plants are messier. Choosing a system depends on response time, process risk, and the detail operators need. A display full of alarms may offer plenty of data, yet still leave workers unsure what to fix first.
Benefits, Challenges, and Integration Considerations
Manufacturing control systems coordinate equipment, people, and production data across a plant. Their value is practical: operators can see machine status, adjust process settings, and respond to faults before small delays spread. A clear dashboard might show a filling line slowing because one sensor reports irregular flow. That matters. Reliable records can also help teams compare shifts, track downtime, and identify recurring quality variation. When controls are well configured, managers can plan maintenance around actual equipment behavior rather than fixed guesses.
Implementation is less tidy. Older machines may use different signals and data formats, while new systems require stable networks, carefully defined access, and tested backups. Integration should begin with a limited production area, mapping each sensor, controller, and data handoff before connecting wider operations. A rushed connection can create duplicate records or misleading alerts. Human factors count, too: an alarm that operators cannot interpret may be ignored, even when the data is correct. Training should use real tasks, such as changing a batch setting or recovering after a stopped conveyor. Security and reliability checks need regular review, not just approval at installation. One uncomfortable lesson is that more data does not always mean better decisions; teams may need to remove metrics that nobody uses.